

Caramel Cooker
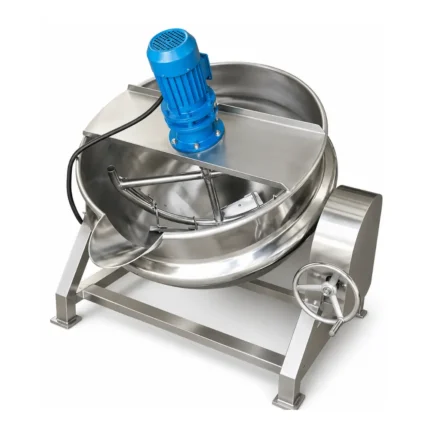
The Caramel Cooker is an industrial food-processing machine designed for efficient cooking, heating, and continuous mixing of caramel and confectionery products. The machine provides controlled processing conditions to achieve a consistent caramel texture, color, moisture level, and cooking quality. Its stainless-steel construction makes it suitable for hygienic confectionery and food-processing applications.
The cooker is suitable for caramel, toffee, fudge, milk caramel, chewy candy bases, confectionery fillings, and other cooked sugar-based products. The robust agitator system ensures effective mixing during cooking and helps reduce product sticking and localized overheating.
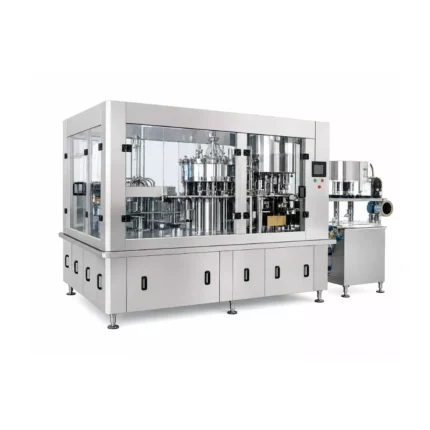
Carbonation Plant
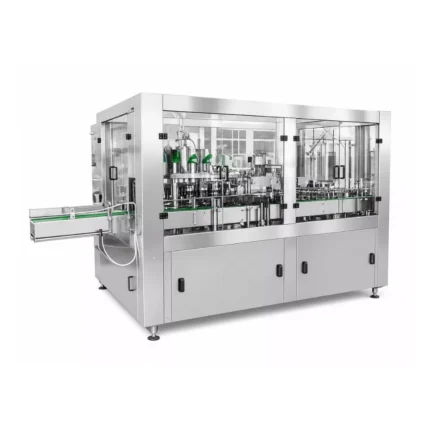
The Carbonation Plant by TRADE SBE is designed for carbonated beverage production and automated bottle filling operations. The machine shown features a stainless steel enclosed structure, a conveyor system, and integrated processing stations designed for beverage packaging. Depending on the selected configuration, the production line can incorporate liquid filling, carbonation-related processing, and bottle capping functions. It is suitable for soft drink manufacturers, sparkling water producers, soda bottling plants, and beverage processing facilities. TRADE SBE offers customized configurations based on production capacity, bottle size, and packaging requirements, along with export packing, shipping support, and installation assistance.

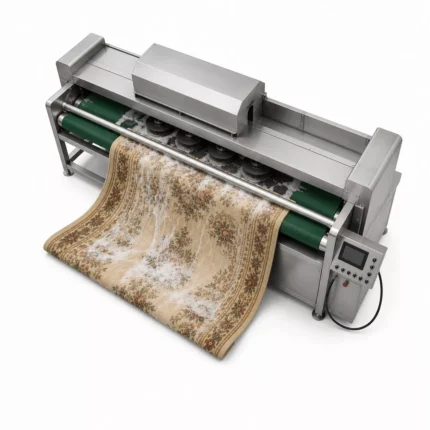


Carton Sealing Machine
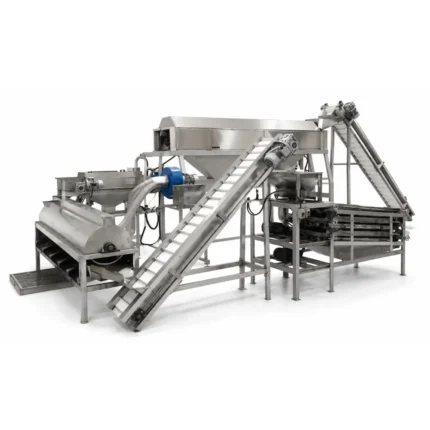
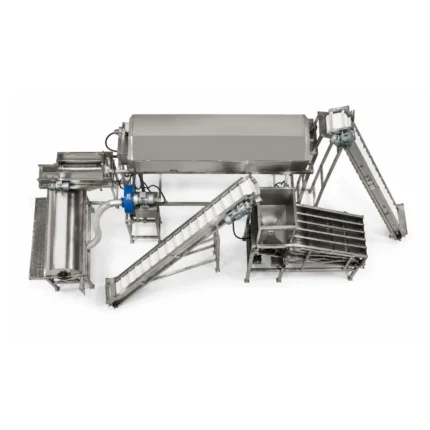
Cashew Processing Plant
A Cashew Processing Plant is an industrial system designed to process raw cashew nuts into market-ready kernels. SBE Trade supplies cashew processing equipment for nut processors, food manufacturers, agricultural businesses, and export-oriented processing facilities. Depending on the configuration, the plant can include cleaning, grading, steaming, shelling, drying, peeling, sorting, and conveying equipment to support efficient production.
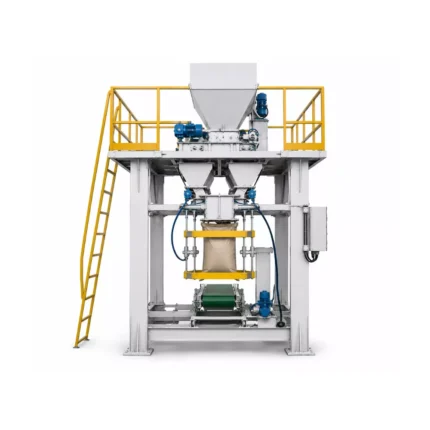
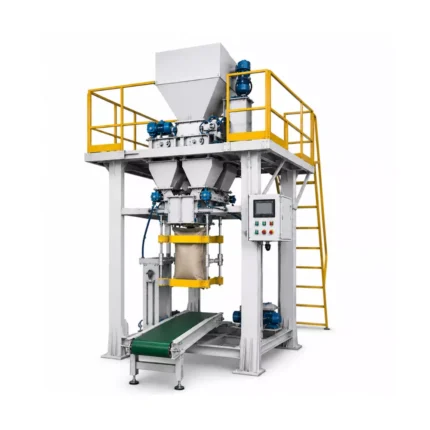
Cement Packing Machine

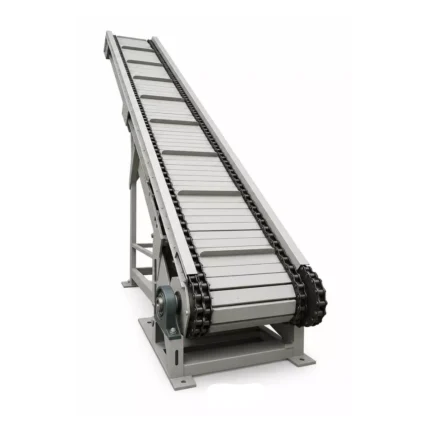
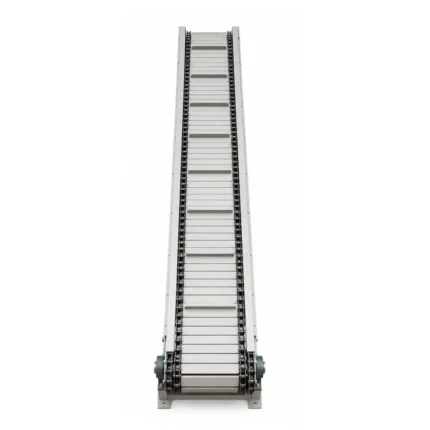
Chain Conveyor
A Chain Conveyor is an industrial material handling system designed to transport heavy products, components, and bulk materials along a defined path. SBE Trade supplies chain conveyor solutions for manufacturing plants, food processing facilities, warehouses, and industrial production lines. These conveyors use a motor-driven chain mechanism to provide reliable material movement and support continuous operations.


Chain Feeding System